Just Purification
Rethinking Single-Pass TFF (SPTFF): The Process vs The Membrane
Why hydraulic operating conditions—not simply cassette configuration—may define the opportunity for high-flux, high-recovery TFF
PROCESS INTENSIFICATION (PI)EQUIPMENT DESIGN
9/27/20266 min read

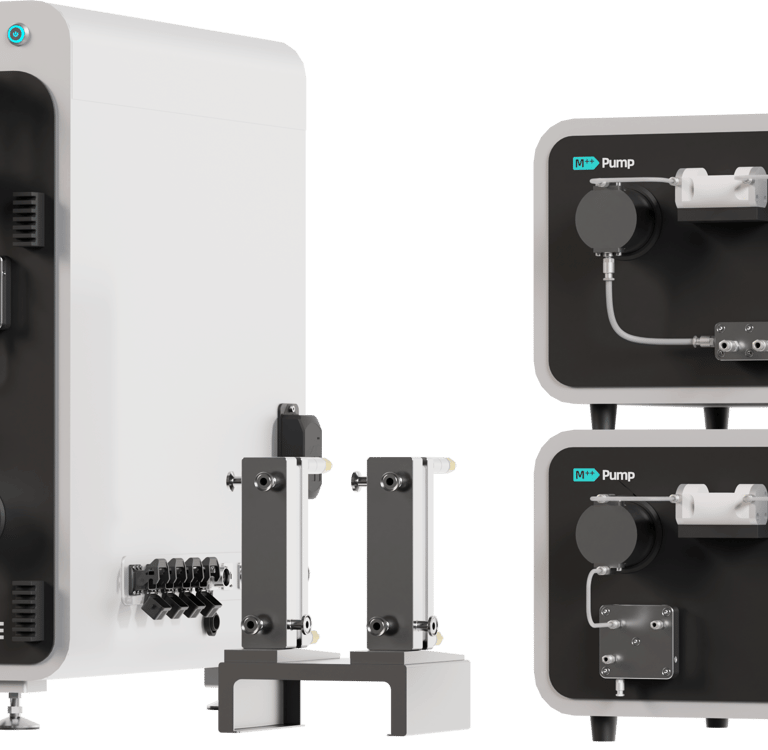
Single-Pass Tangential Flow Filtration (SPTFF) is often discussed as though it were primarily a membrane-device technology: a specially configured cassette, a particular flow path, or a membrane arrangement designed to achieve substantial filtration in a single pass.
Those hardware configurations can certainly be important. But they can also obscure a more fundamental point.
SPTFF is, first and foremost, a process problem.
The central engineering question is not simply how the membrane cassette is constructed. It is whether flow, pressure, membrane area, and filtration conditions can be established and controlled so that the required separation occurs efficiently while maintaining product recovery and product quality.
Looking at SPTFF this way leads to an interesting conclusion: achieving high filtration productivity does not necessarily require operating at high transmembrane pressure (TMP).
Under the right hydrodynamic conditions, high filtration flux can potentially be achieved at relatively low TMP.
That observation challenges some conventional assumptions about how TFF should be operated—and may open a considerably larger operating space for TFF process design.
The Traditional Zone: Pressure And Flux
At its simplest, membrane filtration appears intuitive: TMP provides the driving force across the membrane, so increasing TMP should increase permeate flux.
Within certain operating regions, that is true.
But biological feed streams are not simple fluids flowing through an unrestricted porous medium. As filtration proceeds, retained proteins and other components accumulate near the membrane surface. Concentration polarization develops, and depending on the feed and operating conditions, fouling or a highly concentrated boundary layer may form.
The process can consequently transition from a predominantly pressure-dependent region toward a mass-transfer-limited region.
Once that happens, increasing TMP does not necessarily produce a proportional increase in productive filtration flux. Additional pressure may instead increase the concentration of retained material near the membrane surface and potentially aggravate polarization or fouling.
This is why TMP cannot be considered independently from crossflow.
Tangential flow continuously sweeps the membrane surface. Increasing crossflow can enhance mass transfer away from the membrane and reduce the severity of concentration polarization.
The relevant process question therefore becomes more interesting than simply:
How much TMP can we apply?
A better question is:
What combination of crossflow, TMP, permeate flow, membrane area, and process configuration produces the desired separation most efficiently?
That is why SPTFF is fundamentally a process-design problem.
SPTFF Is Not Defined by a Cassette Alone
A membrane does not inherently “know” whether it is operating in conventional batch TFF, SPTFF, or another TFF configuration.
It responds to its local operating environment: pressure, crossflow velocity, concentration, viscosity, membrane characteristics, permeation rate, and mass transfer at the membrane surface.
This distinction matters.
If SPTFF is treated primarily as a specialized cassette technology, process development can become focused on finding the correct physical membrane arrangement.
But if SPTFF is viewed as an operating strategy, the design space becomes much larger.
The objective is to establish hydraulic conditions under which sufficient filtration occurs during the available membrane exposure while simultaneously protecting yield and product quality.
Hardware remains important, of course. Membrane selection, channel geometry, membrane area, staging, and flow-path design can all affect performance.
But hardware is an enabler of the process—not necessarily the fundamental definition of the process.
In other words:
A cassette configuration does not by itself create an effective SPTFF process. The hydraulic operating conditions established within that configuration do.
High Flux Does Not Necessarily Mean High TMP
This leads to one of the most interesting observations from our TFF development work.
There is a tendency to associate high filtration flux with high TMP. But this relationship can become misleading when filtration is strongly influenced by concentration polarization and mass transfer.
Consider two different strategies.
One strategy attempts to obtain more filtration primarily by increasing TMP.
Another increases crossflow and improves membrane-surface mass transfer while maintaining TMP at a relatively low level.
Under appropriate conditions, the second strategy can provide surprisingly high filtration productivity.
The principle is not that low TMP automatically produces high flux. Nor is high crossflow universally preferable. The optimal operating region depends on the membrane, feed composition, concentration, viscosity, temperature, product characteristics, and separation objective.
The more important point is this:
High filtration flux does not necessarily require high TMP when membrane-surface mass transfer and the overall hydraulic operating condition are properly managed.
This distinction becomes particularly important for protein processing, where maintaining product recovery and quality matters just as much as achieving filtration throughput.
A Different TFF Operating Region
We can think conceptually about several TFF operating regions.
At relatively low crossflow and low TMP, filtration productivity may simply be insufficient.
Increasing TMP can initially increase flux. But as concentration polarization becomes increasingly important, additional pressure may generate diminishing returns.
There is another possibility: operate with substantial tangential flow while maintaining a comparatively low TMP.
In this region, crossflow supports membrane-surface mass transfer while the relatively low TMP avoids relying excessively on pressure as the mechanism for increasing filtration.
This operating region is particularly interesting because it has historically been difficult to access or maintain efficiently with some conventional TFF architectures.
The limitation is not necessarily the membrane.
It can be the way the process is configured and hydraulically controlled.
That distinction has significant implications.
Tankless TFF Provides Another Clue
Tankless TFF provides an interesting example of the same underlying principle.
A conventional batch TFF system normally revolves around a recirculation vessel. Material repeatedly circulates from the vessel through the membrane and returns to the vessel while permeate is removed.
That architecture has been used successfully for decades, but it also establishes a familiar set of relationships among system inventory, recirculation flow, membrane area, feed pressure, retentate pressure, permeate flow, and TMP.
Because engineers have worked within this architecture for so long, its normal operating envelope can easily be mistaken for the inherent operating envelope of TFF itself.
Tankless TFF challenges that assumption.
By changing the process architecture and the way flow and pressure are managed, TFF can be operated under hydraulic conditions that are difficult to realize efficiently in a conventional tank-based recirculation process.
One particularly interesting region combines:
high crossflow + relatively low TMP + high filtration productivity.
Tankless TFF therefore provides useful evidence for a broader hypothesis:
Some apparent limitations of conventional TFF may be limitations of the conventional process architecture rather than fundamental limitations of membrane filtration.
That is an important distinction.
Separating Membrane Capability from Process Architecture
Membrane development has unquestionably driven major advances in bioprocessing. Improved membrane materials, channel designs, cassette configurations, and manufacturing technologies continue to be important.
But membrane performance and process performance should not be treated as the same thing.
A high-performance membrane operated under poor hydraulic conditions can produce a poor process.
Conversely, a well-designed process may extract substantially different performance from an existing membrane by placing it in a more favorable operating environment.
This suggests that TFF development should consider at least two separate questions:
What can the membrane do?
and
What operating environment are we creating around the membrane?
SPTFF brings the second question to the foreground.
Once a large recirculating inventory is no longer assumed to be necessary, flow paths, pressure relationships, membrane exposure, and filtration behavior can be reconsidered.
That creates opportunities for process intensification that do not necessarily depend on inventing a fundamentally new membrane.
Flux Alone Is Not the Objective
There is another important qualification.
The objective of SPTFF should not simply be to maximize instantaneous permeate flux.
A biopharmaceutical filtration process must simultaneously consider yield, product quality, process robustness, and the required separation performance.
Very aggressive hydraulic conditions might generate an impressive instantaneous flux but provide little value if they result in excessive product loss, unstable operation, membrane fouling, or unacceptable effects on the molecule.
The meaningful engineering objective is therefore multi-dimensional:
Achieve the required separation at high practical productivity while maintaining product recovery and quality.
This is another reason SPTFF should be understood as a process rather than a piece of hardware.
The membrane cassette is only one component of the system required to satisfy those objectives simultaneously.
Expanding the TFF Design Space
The larger implication may be that the practical design space for TFF is wider than commonly assumed.
Conventional batch TFF, SPTFF, Steady-State TFF, and Tankless TFF should not necessarily be viewed simply as different equipment categories. They can also be understood as different ways of organizing material flow and membrane hydraulics.
Once viewed from that perspective, several familiar assumptions become open engineering questions.
Does high flux necessarily require high TMP?
Does effective TFF necessarily require a large recirculating inventory?
Must a particular separation objective require a particular cassette architecture?
Or can different combinations of flow, pressure, membrane area, residence behavior, and process configuration reach the same—or potentially better—separation objective?
Our work with SSTFF and Tankless TFF suggests that these questions deserve considerably more attention.
The Process Is the Innovation
The next generation of TFF will certainly continue to benefit from better membranes and better filtration hardware.
But some of the most interesting advances may come from something different: learning how to operate membrane technology in process regions that conventional TFF architectures have made difficult to access.
SPTFF illustrates this point particularly well.
Its defining value should not be reduced to a specialized cassette or membrane cartridge. The real challenge is establishing and controlling the hydraulic environment necessary to achieve the desired separation—with sufficient filtration productivity, high recovery, acceptable product quality, and robust operation.
And one of the most intriguing consequences is that high filtration productivity may not require high TMP at all.
With the right process architecture and hydraulic conditions, high crossflow and relatively low TMP can become a highly productive operating region.
That changes the question from:
“What membrane device do we need for SPTFF?”
to a more fundamental one:
“How should we design the process so that the membrane can perform differently?”
For the future of TFF process intensification, that may be the more important question.